Advantages of laser cutting
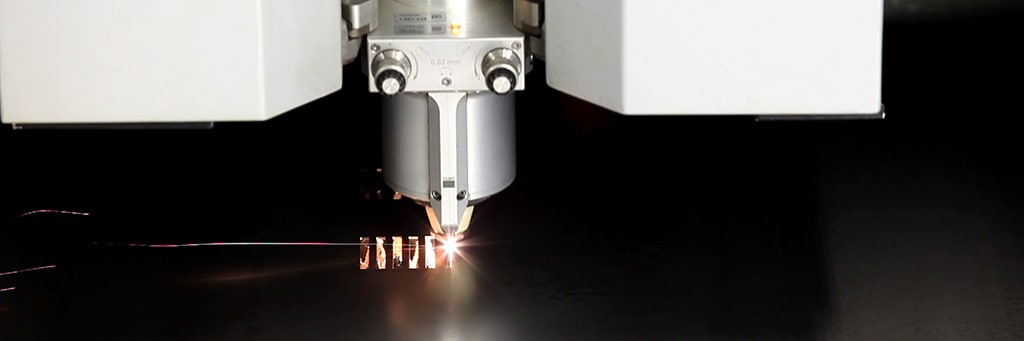
These are the main advantages of laser cutting as a separation technique.
-
Very high degree of freedom of shape
The laser head can follow any desired path at high speed. The shapes that can be produced are therefore not limited to the available punching tools.
-
No burning on the cut edge (oxidation)
When inert nitrogen is used as the cutting gas during laser cutting, it is possible to cut without oxidation discoloration or contamination of the cut edge. Post-processing is therefore usually not needed.
-
No punching transitions
When sheet metal is punched, contours are cut by having the punch head make overlapping punches. This creates a so-called punching transition: a noticeable and sometimes sharp “ridge” on the end product.
-
Limited heat input
A laser beam is a very thin and focused way of cutting, so the thermal deformation of the material is minimal. When making the CAD-CAM program, in which the path of the cutting head is determined, we also take into account the optimal distribution of heat in the sheet to be cut. This allows us to laser cut products with very tight tolerances.
-
Minimal material loss
The width of the laser cut is very thin compared to the minimum diameter of punching tools. The products to be cut can therefore be positioned close together in the sheet they are cut from.
With laser cutting on a flatbed laser with flying optic, there is also no material loss, as there is on a cutting table with a stationary cutting head and clamp strip. If the laser or punch head stays stationary while the sheet is moved, the sheet is usually held by clamps that can move the sheet back and forth. As a result, no cutting can be done within this clamping area. -
High production speed
A laser head can cut a sheet metal product out of the base sheet at high speed. For thicker sheets, the punch-laser combination can also use a single punched hole (not in the end product itself) to reduce the so-called pierce time. The pierce time is the time it takes to cut the first pierce in a sheet. The total pierce time per product can add up quickly for sheets with large numbers of holes. When this piercing is done at high power and high speed in thicker sheets, laser spatter (splashes of molten metal) is created that fuses onto the end product. A pre-punch is an efficient way to start a cutting line without contamination, oxidation and heat input into the sheet.
-
High capacity
Contour’s laser cutting machine can produce unattended outside working hours. The machine can therefore produce unattended and scale up and down quickly to follow our customer’s schedule.
Unattended production is made possible by preparing the programs to be cut in a queue, setting up the laser cutting machine optimally, and using an automatic loading warehouse for sheet material.
-
Laser cutting without microjoints possible
At Contour we can laser cut products without microjoints, even when the products are small. A microjoint is a tiny interruption in the cutting line of the outer contour of a product. The microjoint holds the cut part, as it were, in the larger sheet it is cut from. When the parts are removed, the product is then pushed, pulled or tapped out of the skeleton.
Microjoints are used in sheet metal to prevent the cut products from tilting during cutting and colliding with the cutting head, or falling through the cutting bed and ending up in the cutting waste. A disadvantage of the microjoint, however, is that it leaves a sharp “ridge” on the end product or comes at the expense of subsequent operations or critical tolerances. This means extra post-processing is needed to remove the microjoint.
At Contour we can laser cut without microjoints because we have developed our own finer-mesh cutting bed and make smart use of the CAD-CAM software. If the opening in the cutting bed is still too large and a product can fall through, we can cut small contours with our punch-laser combination. When products are cut loose on this machine, they can fall through a flap under the cutting bed and be collected in a collection bin.